
Calorific Value Measurement and Energy Based Lambda Control
Correlative Gas Analyzer RGQ5
The energy content of the fuel gas is a key process parameter for the stable operation of industrial furnaces. Changes in the supply source or the increasing admixture of foreign gases (e.g. H2, biogas, liquid petroleum gas (LPG, LNG)) lead to significant fluctuations in the calorific value.
As these changes usually occur without the knowledge of the end customer and over undefined periods of time, instabilities in the process are rarely attributed to possible correlations.
By continuously determining the energy content and compensating for it with a tailor-made control concept, it is possible to counteract these fluctuations in a controlled manner.
We recommend RMG's RGQ5 correlative gas quality measuring device.
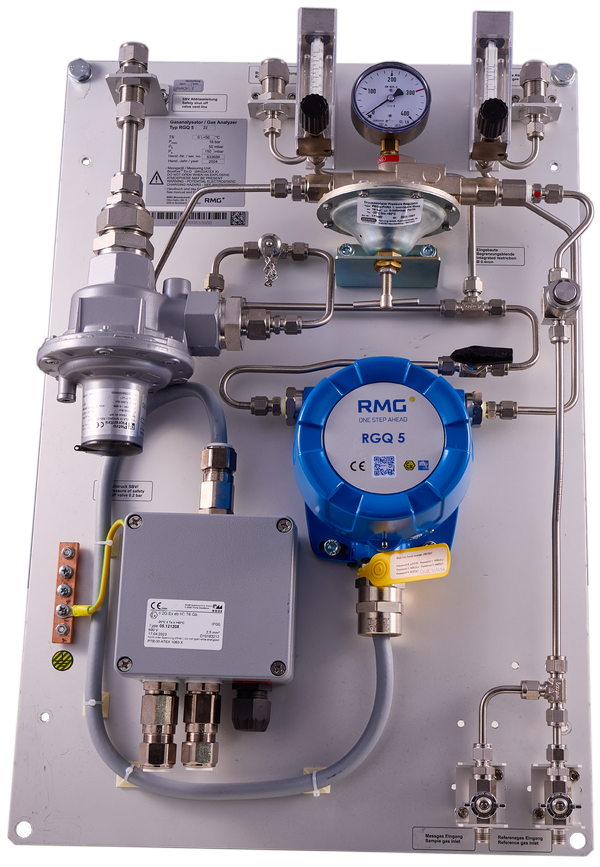
Gas suppliers deliver fuels with varying compositions due to frequent changes of sources of supply
Mixtures of NG with e.g. H2,Biogas, LPG or LNG affect fuel characteristics
This has an impact on
- energy content of gas
- burner’s flame characteristics
- Air / Oxygen demand
Conclusion: A constant energy input is crucial for a stable melting process. The amount of gas alone is no longer sufficient - the fluctuating calorific value must be included in the calculation. The Correlative Gas Analyzer RGQ5 is ideally suited for this.

Reliable online calorific value measurement (correlation method), using a patented gas viscometer technology in combination with additional MEMS sensors
Control of the actual energy input to the process
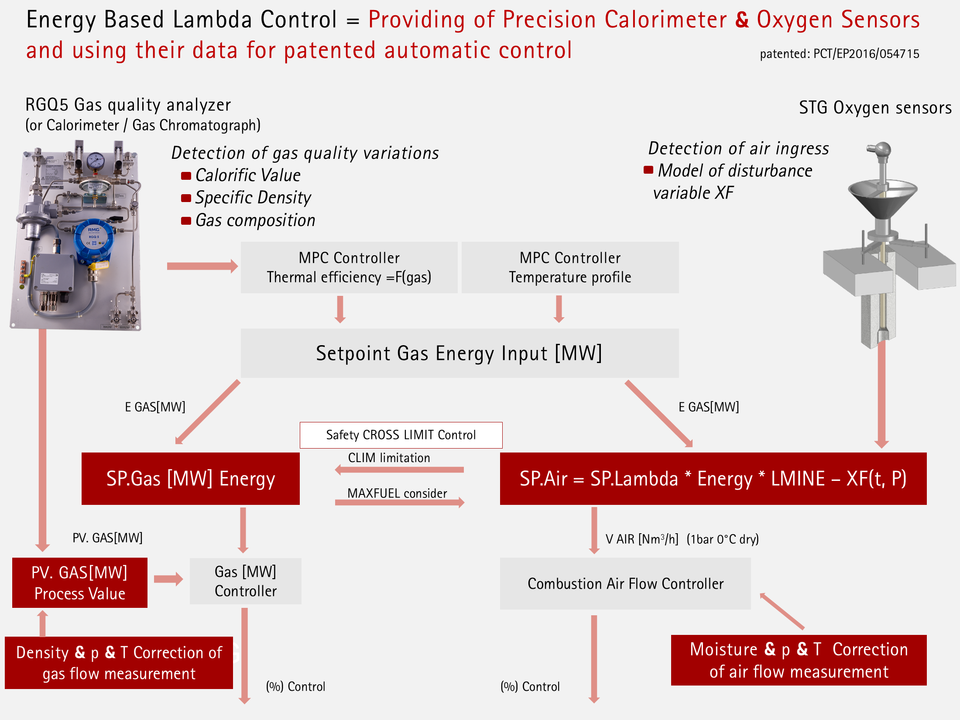
STG Energy based Lambda Control compensates for variations in gas quality by modifying gas flow and combustion air/oxygen setpoints.
Automatic control possible even for short-term variations

Output data:
Continuous measurement of
- Calorific Value (HS & HI)
- Wobbe Index (WIS & WII)
- H2 and CO2 Mol-% (optional)
- Density, Relative density, Compressibility
- Methane number MN
Measuring accuracy:
- Average measurement error < 1% Wobbe Index
- For other gas compositions on request
Maintenance-free and reliable
- No moving parts
- No chemical sensors
Fast and consistent measurement
- Viscosity data every 7 seconds
- Thermal conductivity and CO2 reading every second
Additional features:
- Certified explosion-proof housing
- Built-in gas flow reducer
- Interfaces: 4-20mA, Modbus RTU
- Power supply: 24VDC
- Plug and play installation & operation
- Easy replacement of the sensor unit
- CE, ATEX, IECEx & CSA certificate (optional)
High precision measurement of Calorific Value, Density and Wobbe
No auxiliary gases ( carrier, calibration gases) necessary
No recalibration necessary
A measurement every second
Low cost gas analyzer (compared to typical Gas Chromatograph)
Compact design
Provides all necessary raw data for STG's patented "Energy Based Lambda Control"
Technological consulting
Supplying and installing a complete measuring system with RGQ5 gas quality measuring device.
Signal Processing / Combustion Calculation as an integrated module of the Furnace Control System software provides on-line monitoring of
- Net Calorific value NCV (or: Lower Heating Value LHV)
- Gross Calorific Value GCV (or: Higher Heating Value HHV)
- Wobbe Index
- Stoichiometric air and waste gas flow
- Dimensionless figures of fuel, acc. to Boie
Optional: Patented STG control concept "Energy Based Lambda Control", see below

Energy Based Lambda Control
The ever-increasing problem of unpredictable fluctuations in gas quality over the last few years has created a whole new set of challenges for glass melting plant operators.
In order to counteract the resulting instabilities in the melting process in a controlled manner, STG has developed the "Energy Based Lambda Control" and has been using it successfully for several years.
Calorific value measurement detects changes in gas composition.
STG's oxygen probes react to short term changes in the process and are a reliable indicator to detect uncontrolled air ingress.
STG has combined the advantages of both systems and developed an automatic control feature for a stable energy input into the melting process at all times.
The result (patented) speaks for itself:
Compensation for fluctuations in gas quality and uncontrolled air ingress
Constant energy input (MW) into the melting process
Process stability and constant glass quality
Energy saving (fuel and air)
Reduction of energy losses
Reduction of NOx emissions
Limitation of CO emissions

Available for Siemens / Rockwell (Allen-Bradley) Furnace Control Systems
Patented automatic "Energy Based Lambda Control" for a constant energy input into the melting process:
- Compensation of fluctuations in gas quality
- Compensation of uncontrolled air flow rates
- Maintaining the optimum furnace pressure to prevent air ingress into the furnace
- Calorimeter / Chromatograph monitors the gas quality and provides the control system with the required data for the gas setpoint [MW]
- Oxygen probes provide rapid feedback on changes to the combustion parameters and act as an indicator of the ingress air XF disturbance variable for the control system to correct the required combustion air flow rate
Full integration into visualisation (S7/WinCC; PCS7; iFIX; FactoryTalk)
By modification / extension of existing Furnace PLC and visualisation program (e.g. additional faceplates)
STG requires temporary access to Engineering Station with valid license and currently running program
Installation and Start Up by STG programmer(s) / Optimisation / Support by remote access
Available for Siemens and Rockwell / Allen- Bradley based Furnace Control
- either by extension of an existing Control System
- or as an integral part of a complex Furnace Control System package by STG

For RGQ5 gas quality analyzer get in touch with
Matthias Schuetzel
